Multi-Axis vs 3-Axis CNC Machining: When Does It Matter?
Two shops quote the same part. Both describe themselves as 5-axis capable. One quote is significantly higher than the other. Neither has explained the difference in their approach, and the engineer receiving the quotes isn’t sure what to ask.
This happens because multi-axis vs 3-axis CNC machining gets treated as a capability hierarchy — more axes means better machining. That assumption leads buyers to compare equipment capability instead of comparing how each supplier intends to manufacture the part.
The part’s geometry — not the machine’s axis count — determines the right machining strategy.
What 3-Axis Machining Actually Covers
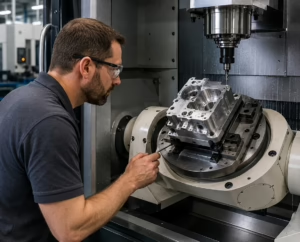
A 3-axis CNC machining center moves the cutting tool in X, Y, and Z with the workpiece stationary. This configuration handles the majority of machined parts: flat surfaces, pockets, slots, holes, standard contours, and any feature accessible from orthogonal directions.
3-axis machining is not an inferior capability. For the right part, it is the correct and economical process. Multiple setups on a 3-axis machine — repositioning the part to machine different faces — are also completely appropriate when the geometry and feature relationships support them.
The question is not whether a supplier has multi-axis capability. The question is whether the part’s geometry and tolerance requirements actually need it.
When Setup Count Becomes a Quality Issue
Three questions help determine whether multi-axis machining is worth considering for a specific part:
How many setups does this geometry require?
How tightly related are features across those setups?
Does the cutting tool need to change orientation continuously while machining a specific surface?
The first two questions matter because every additional setup creates another opportunity for variation in how the part locates relative to previously machined features. When features on different faces have tight positional or geometric relationships, every repositioning can make those relationships harder to control consistently.
At that point, reducing setups may become less about machine capability and more about controlling dimensional risk.
The third question separates 3+2 from simultaneous 5-axis — which is where most of the confusion in supplier conversations begins.
3+2 vs Simultaneous 5-Axis: The Distinction That Changes the Quote
A 5-axis machine can be operated two fundamentally different ways. Understanding both helps explain why quotes from 5-axis shops sometimes differ significantly for similar parts.
In 3+2 positional machining, the rotary axes index the workpiece or tool to a fixed orientation, then remain stationary while X, Y, and Z perform the cutting. This suits angled holes, features on non-orthogonal faces, and multi-face prismatic components where setup reduction adds value without requiring continuous tool-orientation change during the cut. That orientation can also allow shorter, more rigid cutting tools, which can improve stability and access on deep or angled features. Many jobs casually described as “5-axis work” are produced this way.
In simultaneous 5-axis machining, all five axes move during the cut. The tool continuously changes orientation relative to the surface as it travels. This becomes valuable, and in some geometries necessary, when continuously changing tool orientation is required — for continuously contoured surfaces, complex curved geometry, and specific deep-cavity access where the optimal tool angle changes throughout the cut.
Neither approach is universally superior. Many efficient processes use both: 3-axis machining for primary geometry and bulk material removal, with 3+2 or simultaneous multi-axis reserved for the features that specifically require it. The most efficient process may use different machining strategies at different stages of the same part. The machine strategy may even change between roughing and finishing operations on the same component.
More axes are not better. The right setup strategy is better.
Questions to Ask Before the Drawing Goes to Quote
Before a supplier conversation, review the part against four questions:
Are there features on multiple faces with tight positional or geometric relationships between them?
Does the part contain compound angles or continuously contoured geometry?
How many setups would a 3-axis approach require, and where does repositioning introduce risk for critical feature relationships?
Can standard geometry be produced conventionally while multi-axis machining is reserved for features that specifically require it?
The most useful question to ask a supplier is not “Do you have 5-axis?” It is: “How do you plan to manufacture this part?”
That question surfaces the setup strategy, the handoffs between operations, and where the supplier sees variation risk — before any of those decisions are committed to production.
At Borg Design, setup strategy is reviewed during quoting. If the geometry, tolerance relationships, or access requirements suggest a different machining approach than originally assumed, that conversation happens before the process is committed — not after production begins.
For a companion look at specific part geometries that call for 5-axis capability, see When 5-Axis CNC Machining Makes Sense →
Download the DFM Guide
Part geometry decisions — corner radii, wall thickness, datum placement, surface finish — affect which machining strategy a part will need. Borg Design’s DFM Guide covers ten specific design principles for CNC machined parts.
Frequently Asked Questions
Q: When should I ask my supplier about axis strategy?
A: At the quoting stage — before a process is committed. If your part has features on multiple faces with tight positional relationships, angled holes, or continuously curved geometry, raise the question during the initial inquiry. The supplier’s answer reveals how they intend to approach the work and where they see risk.
Q: Is 5-axis machining always more expensive than 3-axis?
A: Not necessarily. Multi-axis machining may carry higher machine or programming costs, but total part cost can be lower when it reduces setup count, handling, variation risk, and secondary operations. For parts that would otherwise require many 3-axis setups, a single multi-axis setup may cost less in total. The right comparison is total part cost, not hourly machine rate.
Q: What is 3+2 axis machining?
A: 3+2 (or positional 5-axis) uses a 5-axis machine but only moves three linear axes during the actual cut. The two rotary axes position the part or spindle to a fixed angle, then lock. Cutting proceeds with standard X, Y, Z motion at that orientation. It is well suited to angled features and multi-face parts where setup reduction is valuable but continuous tool motion is not required.
Q: When is simultaneous 5-axis actually required?
A: When the cutting tool needs to continuously change its orientation relative to the workpiece surface during the cut — typically for continuously contoured geometry, complex curved surfaces, and specific access or surface-finish requirements that depend on maintaining an optimal tool angle throughout the operation.
Q: Why can two 5-axis machine shops quote the same part differently?
Q: Because “5-axis capable” does not describe the actual process. One supplier may use multiple indexed setups, another may use 3+2 positional machining, and another may use simultaneous 5-axis. Tooling strategy, workholding, inspection approach, and how much of the part is completed in each setup can all change the total cost. The machine label is the starting point — the manufacturing process is what determines the number.